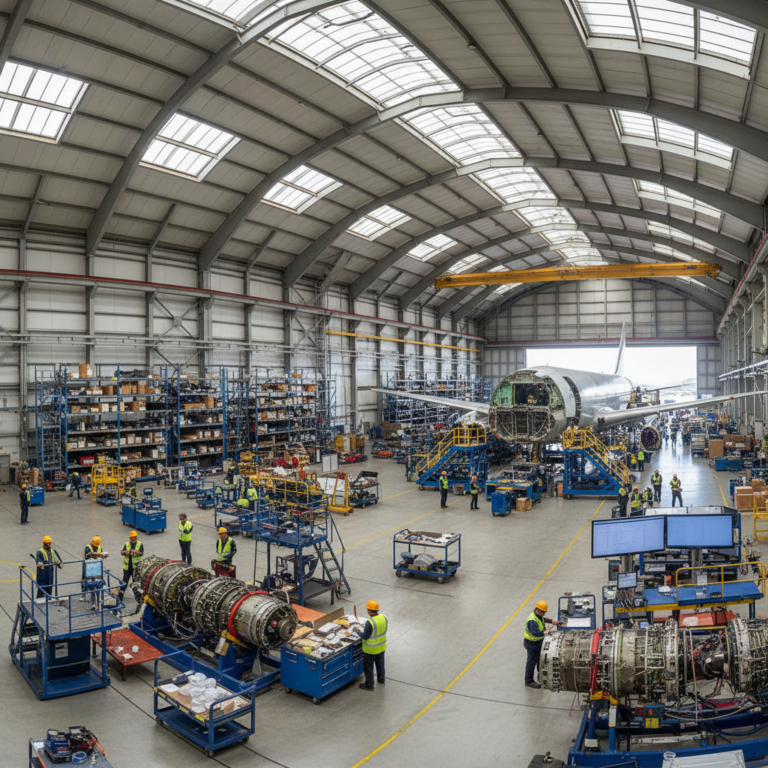
A technician on the A350 final assembly line in Toulouse needs a calibrated torque wrench. It is somewhere in the building. The search takes five minutes. Maybe fifteen. Scale that across thousands of tasks, hundreds of shared tools, and a backlog of 8,754 commercial aircraft waiting to be built, and the real constraint comes into focus. Not a manufacturing problem. A visibility problem.
Real-time tracking in aircraft production does not mean following planes in the sky. It means knowing where tools, components, kits, and work orders are on the factory floor, with enough accuracy and currency to act on that information before the next delay compounds.
Most of what currently ranks for this topic focuses on post-delivery operations: MRO scheduling, fleet management, in-flight telemetry. The production floor, where visibility gaps translate directly into missed delivery targets, gets surprisingly little attention. Having deployed asset tracking systems across aviation supply chains for over fifteen years, I find this is where the ROI case is strongest, and where the risks of getting it wrong are highest.
Why Aircraft Factories Struggle with Visibility
Aircraft assembly is a convergence exercise. Thousands of serialized components from hundreds of suppliers arrive on schedules that rarely align perfectly. Specialized tools are shared between stations. Jobs pause for a missing part, an inspection hold, or a rework correction. The industry tracks every serial number in documentation, but knowing a part exists is not the same as knowing where it is right now, whether it is released for use, and which job needs it next.
The production pressure makes this worse. Airbus delivered 793 commercial aircraft in 2025 (up from 766 in 2024) and targets approximately 870 deliveries in 2026. Boeing delivered 600 commercial aircraft in 2025, its highest annual total since 2018. Both OEMs are ramping rates while managing supply chains that remain fragile. Airbus has cited Pratt & Whitney engine availability as a specific constraint on its A320 program. No tracking system builds a missing engine. But tracking can eliminate the delays factories actually control: the misrouted kit, the tool at the wrong station, the job waiting on parts that are already in the building.
The technology has evolved in stages. A 2008 account described Spirit AeroSystems tracking 30,000 parts at its Wichita 737-fuselage plant using RFID. Airbus deployed location intelligence on its A350 line in 2011. By 2025, Airbus had connected assembly tools to a private 5G network at Hamburg, where tools can be enabled or disabled based on their physical position. The progression tells a clear story: from recording that a part passed a reader, to governing what a tool is allowed to do at a specific station.
What Tracking Solves on the Assembly Line
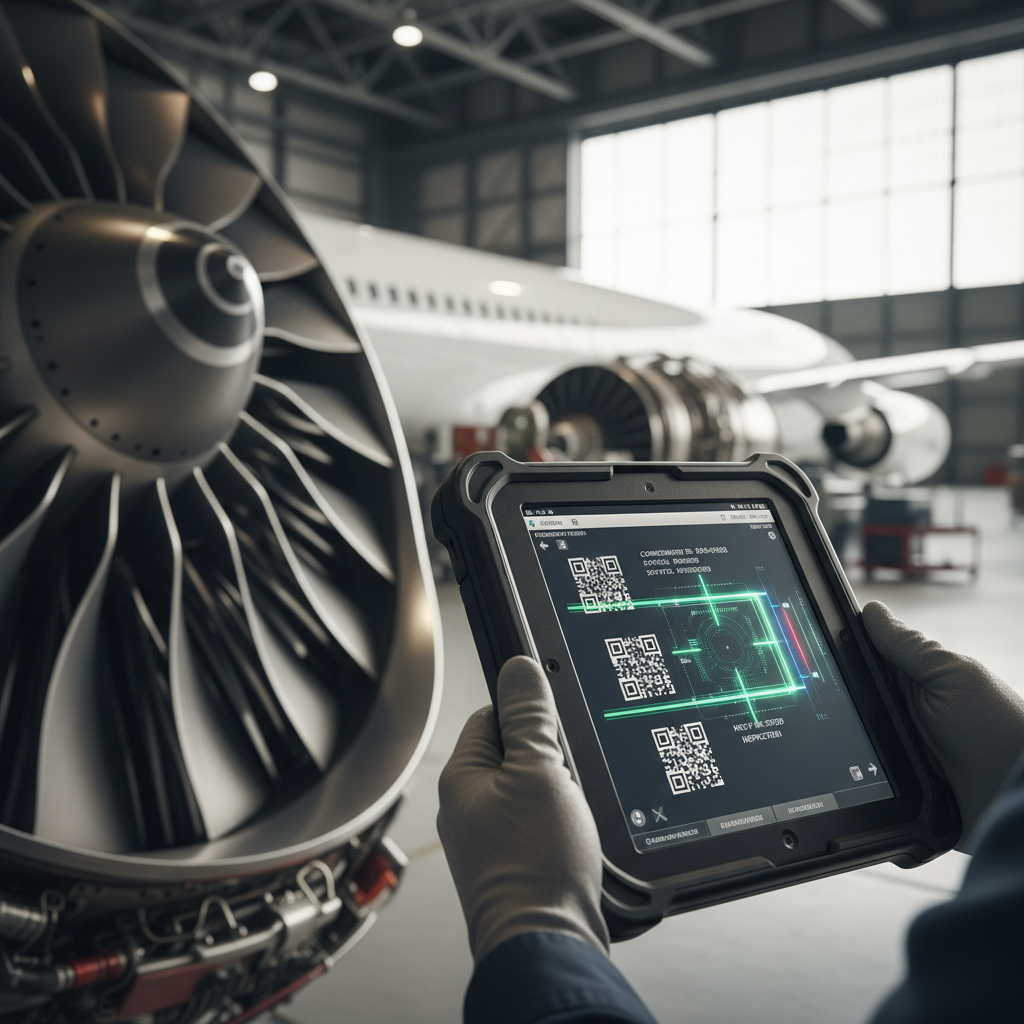
Real-time tracking supports aircraft production through four distinct functions, each building on the last. The published cases illustrate all four, though with varying levels of evidence.
Eliminating search time
The most immediate payoff. A 2026 Litum case study reports 1,800 tracked assets at a European aerospace and defense facility, with search time cut by up to 70% and estimated annual savings near $280,000. At a GE Aviation MRO facility, daily work-order prioritization dropped from three hours per person to 15 to 20 minutes after UWB tracking was deployed. The vendor reports a 12-fold improvement in production-control productivity and a three-month payback.
Both figures are supplier-reported, not independently audited. The GE case is maintenance, not new-aircraft assembly. But the mechanism is the same: if your teams spend part of every shift reconstructing the production queue or hunting for shared tooling, those hours vanish into the backlog every single day.
Preventing wrong-station errors
Finding a tool is useful. Preventing it from being used in the wrong place, with the wrong program, is where safety meets productivity. At Airbus’s Hamburg plant, connected tools on a private 5G network can be remotely enabled or disabled based on geolocation. The correct tool program loads automatically. Torque measurements flow into the MES. A malfunctioning tool triggers an alert before the next use.
The record that matters is not “tool at station B.” It is the verified match between location, authorized program, performed action, and measured result. Airbus says it is still evaluating the full cost reduction and ROI for this deployment, which means the case supports the mechanism more firmly than a universal payback number. But the principle is what counts: location data becomes valuable when it governs what happens next, not just where something sits.
Building the as-built record
Every tag read, scan, or sensor event becomes useful when it links to a part identity, work order, aircraft serial number, and quality disposition. NIST describes this linkage as part of a “digital thread” carrying manufacturing data across the enterprise. GS1’s EPCIS standard provides a framework for exchanging the what, when, where, why, and how of asset events across systems and organizations.
For a Tier 1 supplier shipping serialized components to a final assembler, this creates the difference between “the container arrived” and “the specified component, with its approved status and inspection history, is ready for this job at this station.” One of those statements is a shipping update. The other is a production event.
Connecting the supply chain to the line
Aircraft production does not begin at final assembly. Components traverse multiple supplier tiers, often crossing continents in reusable containers and specialized packaging. Boeing’s December 2025 acquisition of Spirit AeroSystems brought a major fuselage supplier in-house. Most OEMs still depend on external partners for thousands of other assemblies.
This is where production tracking and asset tracking converge. The same logic (identity plus location plus status) that prevents a wrong-program event at a workstation also tells you whether a critical kit left the supplier on time, where your reusable containers are dwelling between cycles, and which inbound deliveries are at risk. If your container pool becomes invisible after handoff, that gap adds cost to every production cycle.
For fundamentals on how location tracking systems operate across different contexts, see how fleet tracking works.
RFID, UWB, or 5G: Picking the Right Approach
The worst procurement mistake in factory tracking is selecting a technology before defining the question it needs to answer. Here is a comparison based on what the published cases actually demonstrate.
| Technology | Best production question | Strength | Key limit |
|---|---|---|---|
| Passive RFID (RAIN) | Which items passed this read point or were found by handheld search? | Low-cost tags, no batteries, high volume | Not continuous location. Missed reads happen, especially around metal. |
| UWB RTLS | Which station or zone holds this tool or transport cart right now? | Frequently updated position estimates (vendors claim 10 to 30 cm precision) | Requires anchors, batteries in tags, site-specific calibration. |
| Private 5G + connected tools | Can the tool receive instructions and return measurements in near real time? | Secure, low-latency communications for tool control and MES integration | 5G connectivity alone is not location. Separate geolocation functions are needed. |
| Barcode / 2D code scan | Was this serialized item deliberately verified at this step? | Direct identity-event record, no RF ambiguity | Requires manual scan. Not continuous. |
Most factories will combine approaches. Airbus uses different technologies at different stages. Boyd, an aerospace and defense supplier, gets adequate WIP visibility from RFID labels on job travelers and handheld readers. MTU Aero Engines chose UWB after testing because its component transport equipment moves through many possible holding areas, making zone-level detection insufficient. There is no single-radio answer.
Site conditions constrain everything. NIST’s guidelines for securing RFID systems warn about interference from metal, unauthorized reads, cloned tags, and network exposure. An aircraft factory full of aluminum structures, composite panels, and electromagnetic interference from assembly equipment is one of the harder RF environments you can deploy in. An RF site survey is not a formality. It is a prerequisite.
The Boeing Door Plug: What Tracking Cannot Fix
In January 2024, a door plug separated from an Alaska Airlines 737-9 mid-flight. The NTSB’s June 2025 investigation found that Boeing personnel had opened the plug to rework rivets, but the four securing bolts were missing before delivery. The required removal record, the document that triggers restoration and quality signoffs, was never generated.
Could a location tag have helped? It could have shown where the plug was on the factory floor. It would not have documented who authorized opening it, which fasteners were removed, whether all four bolts were reinstalled, or who inspected the result. 14 CFR 21.137 requires production certificate holders to control inspection, calibration, nonconforming material, and quality records. The regulation does not prescribe RTLS. RTLS does not satisfy it.
This is the tension most vendor pitches gloss over. Operational speed and regulatory assurance demand different kinds of evidence. Reducing search time is an efficiency gain. Proving that the right work was done by authorized personnel, inspected, and documented is a compliance obligation. A capable tracking deployment serves both. A careless one creates a false sense of control that makes the second problem worse.
The practical response: run two scorecards. Operational metrics (search time, delayed kits, tool utilization). Quality metrics (missing signoffs, wrong-program attempts, unresolved nonconformances). The tracking system that matters is not the one with the most precise dot on the map. It is the one that triggers the correct next action without weakening the controls that make an aircraft releasable.
How to Evaluate the Investment
Every RTLS vendor will show you a compelling dashboard. Fewer will help you build the baseline that proves the system works in your facility, not theirs. Before signing anything, measure what you have now:
- Average and worst-case search time per shift for tools, parts, and work orders
- Number of late or incomplete kits per week
- Tool utilization versus tool availability across shared equipment
- Wrong-station or wrong-program events per month
- Labor hours spent rebuilding the production queue each morning
After deployment, validate against those baselines. “Up to 70% search-time reduction” and “12x productivity improvement” are useful reference points from other facilities, but your results will depend on layout, shift patterns, metal density, and the quality of your MES integration.
Questions worth asking any prospective vendor:
- What location accuracy does this specific workflow actually require? (A kit staging area and a fastener installation point are not the same question.)
- How does the system handle missed reads, RF interference, and offline operation?
- Which MES and ERP records does it write? Who retains authority to change a quality status?
- How will we validate outcomes against our baseline, not a reference customer’s demo environment?
- What cybersecurity controls protect tag data, reader access, and network interfaces?
For tracking challenges that extend beyond the factory floor (components in transit, reusable containers between supplier sites, ground support equipment on the ramp), the technology stack changes but the logic stays the same: identity, location, status, next action. Our team at Datanet works across the aviation supply chain, from DO-160 approved airfreight trackers to rugged industrial asset tracking devices built for the environments between factories. If that is the conversation you need, reach out.
Frequently Asked Questions
Does real-time tracking in aircraft production mean tracking planes in flight?
No. In a production context, it means locating tools, components, kits, and jobs on the factory floor with enough currency to drive the next operational action. Flight tracking via ADS-B, ACARS, or satellite is a separate system for aircraft already in service.
Does the FAA require real-time location systems in factories?
No. 14 CFR 21.137 requires production certificate holders to maintain controls over inspection, calibration, nonconforming material, and records. It does not prescribe RTLS as the means of compliance. A location system can support those processes but cannot substitute for them.
Which technology is best for aircraft factory tracking?
It depends on the question being answered. Passive RFID identifies items at read points. UWB provides more continuous, precise positioning. Private 5G carries tool commands and MES data. Most factories combine multiple technologies matched to the accuracy and update frequency each workflow actually requires.
What ROI should manufacturers expect?
Published vendor cases report up to 70% reductions in search time and three-month payback periods, but these are facility-specific results. Measure your own baseline (search hours, late kits, queue-rebuild labor) and validate improvement against it. Airbus itself says it is still evaluating the full ROI of its Hamburg connected-tools deployment.
Can a tracking tag prove a part is safe to install?
No. A tag can identify or locate an item. Conformity requires approved design data, documented status, authorized disposition, and inspection. The NTSB’s Boeing 737-9 door-plug report demonstrated the consequences of a missing removal-and-restoration record, regardless of whether the part’s physical location was known.
How large is the RTLS market for aerospace production?
No reliable aerospace-only figure is publicly available. The all-industry RTLS market was estimated at $6.68 billion in 2025, projected to reach $15.67 billion by 2030 according to MarketsandMarkets. That total spans healthcare, logistics, retail, and manufacturing. Treat it as directional context, not an aerospace-specific forecast.


 +1 508 292 2210